meridsource White Logo

How to Build an Operating System When Your Product Line Starts Growing

Launching one product is mainly a product development challenge.

Building a collection of products becomes an operational challenge.

This is a transition many growing bag brands underestimate.

At the beginning, the main goal is simple:

Create a product customers want.

But as the product line expands, the business requirements change.

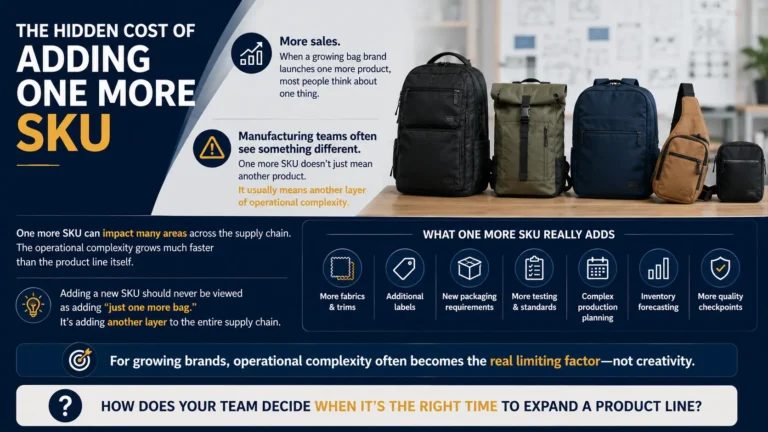
More products create more connections between different parts of the operation.

1. Create Structure Before Adding More Products

When a brand manages multiple products, every decision can affect the entire product line.

A new product may impact:

  • Material sourcing.
  • Supplier coordination.
  • Production planning.
  • Packaging requirements.
  • Inventory management.

Without clear systems, small decisions can create larger operational problems.

2. Build Shared Product Standards

Growing brands need consistency across products.

This includes:

  • Material specifications.
  • Quality standards.
  • Packaging guidelines.
  • Production requirements.
  • Documentation processes.

Shared standards make it easier to manage multiple SKUs and maintain product quality.

3. Improve Coordination Across the Supply Chain

As collections grow, production becomes more connected.

Different products may compete for:

  • Factory capacity.
  • Material availability.
  • Development resources.
  • Quality control attention.

Better planning helps brands avoid delays and unnecessary complexity.

4. Recognize When Product Development Becomes Operations Management

A growing product business is no longer only about creating new designs.

It becomes about managing a system that connects products, suppliers, materials, and processes.

Successful brands understand this transition early.

They build operational systems that allow creativity to continue without creating unnecessary complexity.
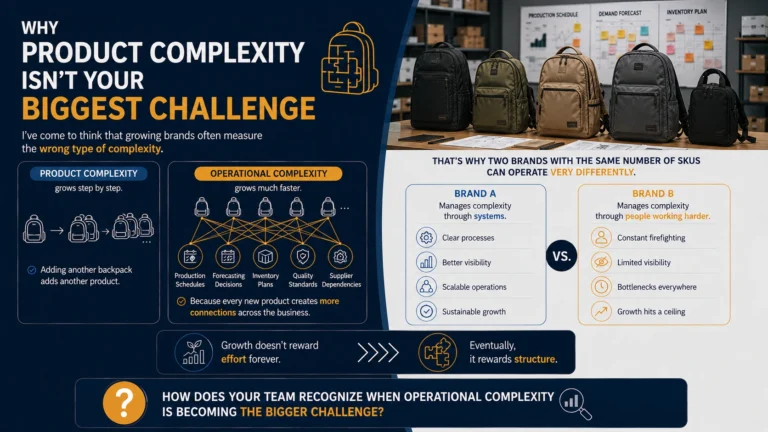
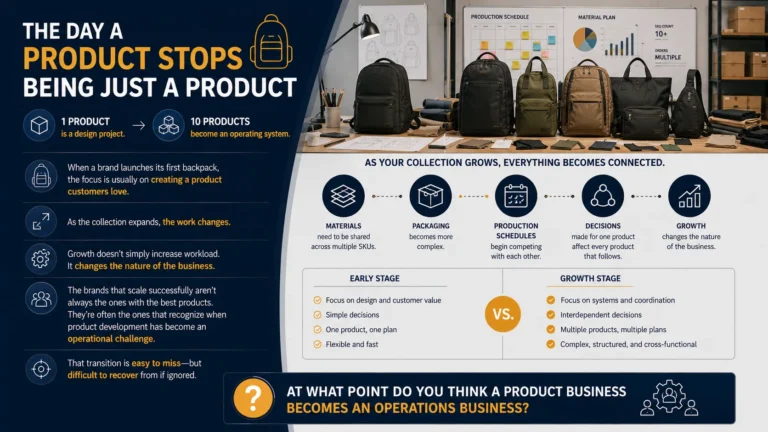
Growth does not only increase the number of products.

It changes how the business needs to operate.

Latest knowledge

FAQs

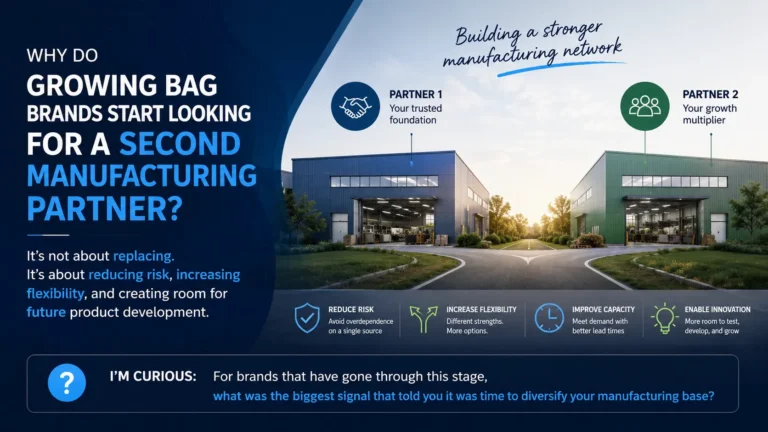
A brand should evaluate a second manufacturer when it can identify a specific capacity, capability, concentration, lead-time, or geographic constraint. The decision should be supported by a clear product allocation model and controlled requirements. A general desire for “more options” is not enough. First confirm that the real problem is not late planning, changing specifications, weak forecasting, or unclear internal ownership.

No. Dual sourcing can reduce dependence on one production route, but it also creates more coordination, qualification, documentation, material, and quality-control work. Two factories may still depend on the same upstream supplier. Risk falls only when the second route is genuinely qualified, addresses the relevant dependency, and can be managed without creating larger execution problems.

Sometimes, but only when the business exposure justifies planned dual sourcing. Both factories need controlled specifications, approved materials, patterns, tooling rules, quality criteria, and comparable production evidence. For many brands, a capability split is simpler: each factory owns a different product family. The correct model depends on the risk, volume, and management capacity.

Start with a controlled pilot SKU that tests the capability the brand actually needs. Review similar-product evidence, technical communication, material control, sampling, pre-production preparation, inline quality, final inspection, packaging, and delivery. Then place a limited pilot order. Do not qualify a production partner from a showroom, quotation, audit, or single sample alone.

Use one controlled product standard. It should include the tech pack, BOM, approved material and color references, construction details, tolerances, tests, packaging, approved sample, and inspection criteria. Use the same change-control and corrective-action process for both factories. Even with these controls, compare real production output because different equipment, materials, and workmanship can still create variation.

The reaction often depends on how the change is managed. Explain the business reason, protect confidential information, and keep allocation criteria stable. Do not frame a strategic network decision as punishment when the supplier has performed well. If the current factory continues to receive meaningful, well-planned business, the relationship can remain strong while the brand adds another capability or continuity route.

Often, it is not. Dividing limited volume can reduce leverage and attention at both factories. A qualified backup for one selected product may be more practical than two active sources for every SKU. Before adding a factory, compare the value of diversification with the extra development, MOQ, material, quality, travel, and management cost.